
The same hoodie, ordered twice at different volumes, behaves like two different projects. At a hundred pieces the fabric is usually taken from what exists, the decoration setup is spread across very few units, and the sampling cost is a visible share of the total. At a thousand pieces the fabric may be produced to order, the cutting method changes, and the fixed costs stop mattering while the risks move to consistency. Understanding which costs are fixed and which are variable is what makes the volume decision a commercial one rather than a guess.
What actually changes when a hoodie order moves from 100 to 1,000 pieces
Four things change when a hoodie order grows from 100 to 1,000 pieces: the fabric route, the cutting method, the decoration setup and the packing and freight configuration. Only one of them, the fabric, usually lowers the unit price; the rest decide how predictable the order becomes.
Four things change, and only one of them is the unit price. The first is the fabric: a small order usually takes what is available, while a larger one can justify dyeing or knitting to the specification. The second is the cutting method, because a marker that is inefficient at low volume becomes practical at higher volume. The third is the amortisation of fixed costs — sampling, grading, decoration setup — across more units. The fourth is the intensity of inspection and packing, which can be increased at volume because the cost per unit of doing so falls.
The risk profile also shifts. At low volume the principal risk is paying too much per unit and discovering that a fixed cost could not be spread. At high volume the principal risk is consistency: a specification error or a fabric variation repeats across a thousand garments rather than a hundred, and the cost of correcting it scales with the order.
| Element | At low volume | At higher volume |
|---|---|---|
| Fabric | Taken from what is available | Can be dyed or knitted to specification |
| Cutting | Manual lay, simple marker | Marker optimisation and higher-yield methods |
| Decoration setup | Large share of the per-unit price | Spread thinly across the run |
| Sampling | Visibly expensive per unit | Absorbed by the order value |
| Inspection | Often final inspection only | In-line checks become affordable |
| Freight | Less than full container, higher per unit | Consolidated, lower per unit |
Fabric: stock fleece versus custom-dyed and custom-knit
At low volume the fabric decision is usually constrained rather than chosen. A colour outside the stocked range means a dye lot with its own minimum, which can exceed the quantity of the order. That is why small runs tend to stay inside the available colours and weights, and why a brand that wants a distinctive colour usually has to accept either a larger first order or a stock colour.
At higher volume the fabric becomes a specification rather than a constraint. Dyeing to a reference, knitting to a chosen weight, and specifying the surface treatment all become practical, and the fabric cost per unit is negotiated against a real volume rather than a minimum. The trade-off is lead time: a produced fabric adds weeks to the calendar that a stock fabric does not. The two wholesale references for this decision are weight and construction, covered in this guide to hoodie weight and GSM and this comparison of fleece and French terry.
Cutting: manual versus die and CNC cutting economics
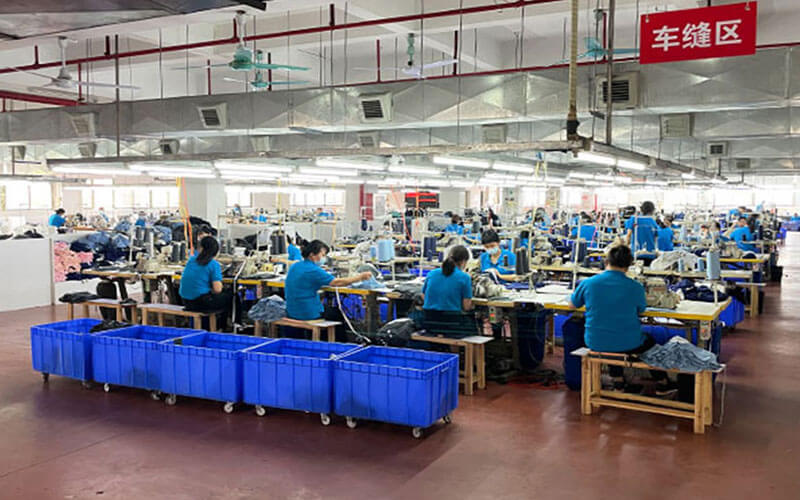
Cutting is where volume changes the method rather than only the cost. At low volume a small lay is cut by hand or with a simple straight knife, which is flexible and requires no tooling but produces more variation between pieces and leaves more material unused. At higher volume the marker can be optimised, the lay can be deeper, and automated cutting becomes economical because its setup cost is spread across more units.
The practical consequences for the buyer are yield and consistency. A better marker reduces consumption, which reduces the fabric cost per garment; a deeper lay or an automated cutter reduces the variation between pieces, which matters most on a garment with a dropped shoulder or a heavy fabric where a small deviation is visible. Buyers moving a style from a small run to a larger one should expect the supplier to change the cutting method, and should ask how consumption is calculated at each volume rather than assuming the figure carries over.
Printing and embroidery setup amortisation per unit
Decoration setup is the clearest example of a fixed cost that behaves badly at low volume. A screen print carries a setup per colour per position; embroidery carries a digitising charge per design; an underbase for a light print on a dark garment adds a further screen. None of these costs changes with quantity, so at a hundred pieces they can represent a large share of the unit price and at a thousand pieces they almost disappear.
Two consequences follow. The first is that a reorder of the same design is materially cheaper per unit than the first order, provided the setup is charged per design rather than per run; that distinction should be established at quotation. The second is that decoration choice is partly a volume decision: a design that is uneconomic at low volume may be entirely reasonable at higher volume.
Sampling and approval overhead per unit
Sampling cost is fixed in the same way. A pattern, a grade and a set of sample rounds cost the same whether the eventual order is small or large, so the per-unit burden falls as volume rises. That is why a first small order always carries a higher effective unit cost than the reorder that follows it, even when the garment specification is identical.
Buyers should treat the sample cost as part of the development asset rather than as a per-order expense. The pattern and the grade created during sampling are reused on every subsequent order, so the cost is amortised across the life of the style rather than across the first run. Where a supplier credits part of the sample cost against a first bulk order, that credit is a pricing decision rather than a reduction in the underlying cost.
QC method and inspection intensity at each volume
Inspection intensity is a volume-dependent choice, and this is one of the few places where a larger order gets better treatment. At low volume a final inspection is often the only practical option. At higher volume it becomes affordable to check in-line, which catches a systematic problem while it is still correctable rather than classifying it at the end.
The checks worth adding at volume are the ones that predict returns: seam integrity and stitch density on a heavy fabric, hood and pocket attachment strength, zipper function where applicable, and shrinkage after the intended care regime. Testing houses publish the scope they apply to knit garments, as Intertek’s textiles and apparel testing range illustrates, and the ASTM standards programme for textiles provides neutral vocabulary for describing the property under test.

Packaging, cartons and freight consolidation
Hoodies are bulky, so packing decisions have a larger freight consequence than they do on a light garment. At low volume the carton plan is usually whatever fills the cartons reasonably, and the shipment may move as less than a full container, which raises the cost per unit. At higher volume the carton plan can be designed for the container or pallet configuration, and the shipment consolidates.
Three specifications decide the outcome: the fold, the bag, and the pieces or weight per carton. A change to the fold standard changes the carton count and therefore the freight calculation, which is why the packing specification should be fixed before production rather than at shipment. Where a delivery term is quoted, it should be named explicitly, because the ICC Incoterms rules define where cost and risk transfer and a quotation without a term cannot be compared with another.
Reorder and restock behaviour at each volume
Small orders and large orders also behave differently after delivery. A small first order tends to sell through quickly if the style works, which means the reorder window arrives before the fabric and capacity are guaranteed. A large order creates stock that has to be worked through, which means the next order is planned rather than reactive, and the risk is overstock rather than stockout.
The practical difference is the trigger. A small-volume programme needs a reorder trigger set against sell-through and against the lead time of its fabric and decoration, because a made-to-order colour cannot be replaced quickly. A larger programme can reorder on a planned cycle, where the constraint is cash and warehouse space rather than production lead time. Buyers should write the trigger into the programme rather than discovering it in a stockout.
Deciding the right volume for a first season
The decision usually comes down to how much of the fixed cost a brand is willing to carry to learn something. A smaller first order pays more per unit in exchange for a shorter commitment and a faster read on demand; a larger first order lowers the unit cost and requires more confidence in the specification, because a mistake repeats across more garments.
Three questions make the trade-off concrete. Is the fabric available in the required colour at the smaller quantity, or does a dye lot force the volume up? Does the decoration carry a setup that only makes sense at higher volume? And is the specification close enough to proven that a repetition of an error would be tolerable? Where the answers point in different directions, the usual resolution is a smaller first order on a stock fabric with simple decoration, followed by a larger order once the style and the specification have both been validated. Buyers who plan the second order at the same time as the first get the benefit of the smaller commitment without losing the volume economics on the reorder.

Conclusion
Volume does not simply change a price; it changes the fabric route, the cutting method, the inspection intensity and the freight configuration. Fixed costs — sampling, grading, decoration setup — behave worst at low volume, while consistency risk grows with the order. That is why a smaller first order on a stock fabric with simple decoration is often the cheapest way to validate a specification, and why the reorder that follows it can be materially cheaper per unit. Buyers who separate fixed from variable costs at quotation, and who decide the volume against the fabric availability and decoration setup rather than against price alone, get a programme that scales without rebuilding itself. Where a facility or social audit is also required, amfori administers the BSCI framework many European buyers reference, and where a delivery claim depends on the transport mode, the International Air Transport Association’s cargo programme publishes the applicable handling standards.
FAQ
Why is a reorder cheaper per unit than the first order?
Because the fixed costs – pattern, grading, sampling and decoration setup – are incurred once and spread across the order quantity. Whether the reorder carries a fresh setup depends on whether the supplier charges setup per design or per run, which should be established at quotation.
Does a larger order always mean a better price?
The unit price usually falls, but the total commitment rises and the consistency risk scales with the order. A pattern error or a fabric variation repeated across a thousand garments costs more to correct than the same error across a hundred.
When should we accept a dye lot to get our colour?
When the colour is central to the range and the quantity justifies the minimum, or when the programme can absorb the lead time a produced fabric adds. Otherwise a stocked colour keeps the first order smaller and gets the style to market sooner.
What changes in inspection as volume rises?
In-line checks become affordable, because their cost is spread across more units. That matters because a systematic problem caught in-line can be corrected, while the same problem found at final inspection can only be classified.
Next step. If you are deciding between a test run and a larger first order, send the style and the volume you are considering. The team can confirm which fabric route each volume allows, how the decoration setup behaves at each size, and what the packing plan would produce in freight terms.
